China has become a major production base for plastic parts used in automotive, electronics, medical, packaging, and industrial equipment. For global buyers, selecting a capable manufacturer requires more than comparing prices. The right partner should understand material behavior, mold design, injection parameters, surface finishes, and international quality expectations. This guide examines ten Chinese manufacturers serving overseas customers. It focuses on practical capabilities, including engineering support, tooling control, production capacity, inspection systems, and export experience. Factory visits, production records, and customer-facing evidence matter. So do clear communication and documented processes. A polished website is not enough. Neither is a low quotation. Each manufacturer profile should explain its strengths, typical applications, equipment, certifications, and ability to manage custom orders. We also consider how suppliers handle sampling, dimensional checks, packaging, and delivery coordination. These details often reveal more than promotional claims. They show whether a supplier can support stable production instead of one successful trial.
However, no supplier list can replace buyer-side verification. Capabilities change, equipment ages, and certification scopes may not cover every product. Some published information can also be incomplete or difficult to compare. That uncertainty deserves attention. Readers should request current certificates, material datasheets, inspection reports, and production samples before making commitments. Ask for references where appropriate. Request a clear quotation with tooling, tolerances, lead times, and quality responsibilities. Confirm who owns the mold. Review communication during the early technical discussion. This article offers a structured starting point, not a final verdict. It helps procurement teams identify credible options while recognizing their own technical requirements and risk tolerance. Whether you need a small precision component or high-volume molded assemblies, reliable sourcing begins with evidence, careful questions, and realistic expectations. Good decisions take time.
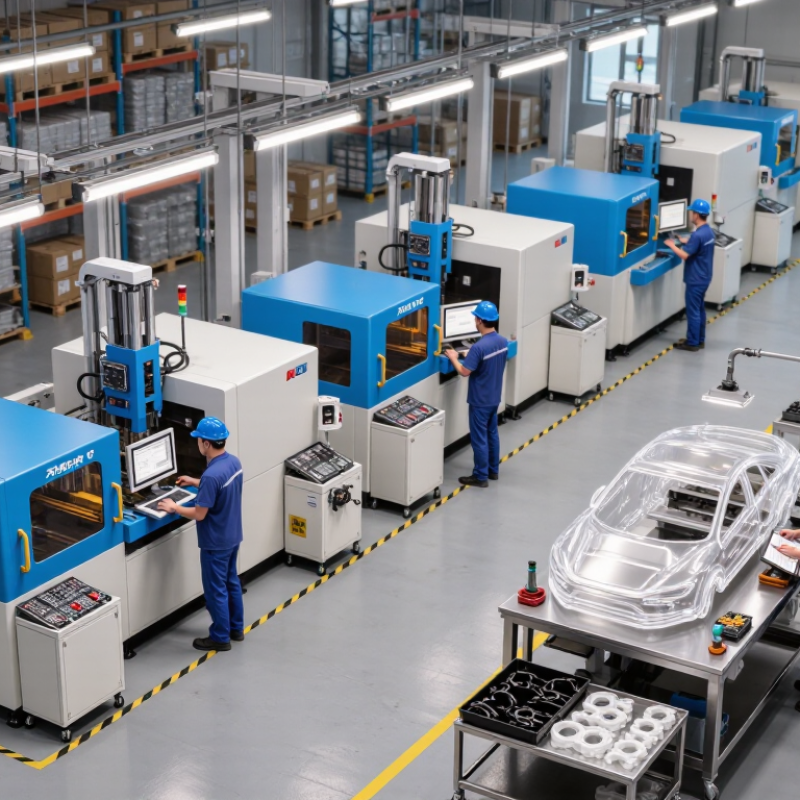
China’s plastic parts sector exceeded 74 million tonnes of output in 2023, according to industry data. This scale reflects deep manufacturing capacity, broad material access, and mature processing networks. For global buyers, it creates more sourcing options across automotive, electronics, medical equipment, packaging, and industrial applications.
High output does not automatically mean consistent quality. A factory may produce thousands of parts daily, yet struggle with warpage, color variation, or weak dimensional control. Experienced buyers should review mold design, resin specifications, inspection records, and production samples before placing large orders. Small details matter. A 0.2-millimeter deviation can affect assembly.
China’s leading plastic parts manufacturers often support injection molding, precision machining, overmolding, and custom tooling. Many also use automated inspection, in-process testing, and traceability systems. Buyers should request measurable evidence rather than rely on polished presentations. Material certificates, tolerance reports, capability studies, and sample approval records provide stronger assurance.
The sector’s size can shorten lead times and improve cost efficiency, but it may also encourage rushed supplier selection. That is a real risk. Some factories look capable during a sample run but perform less reliably during mass production. Regular audits, clear technical drawings, and staged inspections can reduce this gap. Environmental performance also deserves closer attention, especially when recycled content or production waste affects product consistency.
China remains a major base for plastic parts manufacturing. PlasticsEurope reported global plastic production of 413.8 million tonnes in 2023, with China contributing about 32%. That scale supports strong tooling, injection molding, and export infrastructure. However, capacity alone does not prove reliability.
For global buyers, the top 10 manufacturers should be ranked through measurable evidence. Production capacity shows whether suppliers can support repeat orders. MOQ reveals flexibility for testing and smaller launches. ISO 9001, ISO 14001, and sector-specific certifications indicate process control, but certificates require verification.
Export data from UN Comtrade and China Customs can reveal market experience across several years. Buyers should also check mold ownership, dimensional inspection records, material traceability, and average lead times. Public data is sometimes incomplete. That deserves caution.
Tips: Request audited capacity figures, recent export records, and sample inspection reports. Compare quotation terms carefully. A low MOQ may hide higher tooling costs. Ask for tolerance data, not only catalog photos. Independent factory audits remain useful, although they add time and expense. In practice, the “best” supplier may not have the largest plant. A smaller facility with stable quality can perform better. This ranking method is useful, but it is not perfect. Supplier conditions change quickly.
China Top 10 Plastic Parts Manufacturers for Global Buyers
Global buyers often compare plastic parts manufacturers by process capability, not catalog size. Injection molding suits repeat production, tight tolerances, and complex ribs. Engineers should check gate marks, draft angles, wall thickness, and mold maintenance records. A small warpage issue can stop an assembly line. Details matter.
CNC machining supports prototypes, low-volume parts, and materials requiring accurate cuts. It also exposes design weaknesses early. Ask for dimensional reports and inspect critical holes with calibrated gauges. Blow molding works well for hollow containers, ducts, and tanks. Uneven walls remain a common concern, especially near corners. The sample may look acceptable, yet fail during pressure testing.
3D printing helps validate shape, airflow, and assembly before tooling costs begin. Different printing methods create different surface textures and strength levels. A printed prototype is not always a production reference. This point is easy to overlook. In practical supplier evaluations, clear process records often matter more than polished presentations. Buyers should review material certificates, inspection plans, tooling ownership, and corrective-action evidence. I would also question overly perfect claims. Real factories usually have rejected parts, process adjustments, and lessons learned. That transparency can reveal stronger quality control than a flawless report. Precision comes from repeatable methods, trained technicians, and honest communication.
Typical lead time for receiving the first production-ready parts, based on common manufacturing workflows for global buyers.
Injection molding and blow molding generally require additional tooling, while CNC machining and 3D printing can begin with minimal or no dedicated tooling. Actual timing depends on part complexity, material, quantity, surface finish, mold design, and quality requirements.
Global buyers evaluating China’s top plastic parts manufacturers should examine evidence, not polished catalogs. ISO 9001 shows a controlled quality system, but it does not guarantee every molded part is perfect. Ask for audit scope, corrective-action records, and recent process data. At the factory, verify calibrated gauges, resin lot labels, and inspection points beside molding machines. Small details matter.
For automotive work, IATF 16949 indicates stronger process discipline and risk control. It should connect with control plans, PFMEA reviews, capability studies, and traceability from pellets to packed parts. PPAP is equally practical. Request samples, dimensional results, material records, appearance standards, and signed approval evidence before mass production. A complete file should match the actual tool, cavity, resin, and revision.
RoHS and REACH support safer material selection and international compliance. However, a declaration alone can be weak. Buyers should check supplier statements, laboratory reports, and change-control procedures. Ask what happens when resin or colorant changes. It is not always smooth. Some factories may show excellent first-article results yet struggle with weekly consistency. Independent inspections, retention samples, and clearly agreed acceptance limits expose that gap early. Experienced sourcing teams also review response times, not only certificates. A fast, honest explanation of a defect often reveals more than a perfect presentation.
| Benchmark Profile | Primary Manufacturing Region | Typical Plastic Part Focus | Common Material Scope | Typical Part Weight Capability | Typical Tolerance Benchmark | ISO 9001 | IATF 16949 | RoHS / REACH Support | PPAP Capability | Recommended Buyer Verification |
|---|---|---|---|---|---|---|---|---|---|---|
| Profile 01 | Pearl River Delta | Precision automotive interiors, clips, brackets, and functional housings | PPABSPC/ABSPA66 GF | 0.5–800 g | ±0.05–0.15 mm* | Required | Preferred | Material declarations and test reports | Levels 1–5 available by project | Audit certificate scope, mold-flow report, Cpk data, and automotive customer references |
| Profile 02 | Yangtze River Delta | Electronic enclosures, connectors, sensor covers, and thin-wall components | PCPBTLCPPA | 0.1–500 g | ±0.03–0.10 mm* | Required | Sector-dependent | RoHS declarations; REACH SVHC review | Available when automotive content applies | Check resin traceability, UL-related material records where relevant, and dimensional GR&R |
| Profile 03 | Pearl River Delta | Consumer appliance panels, knobs, bezels, and cosmetic molded parts | ABSHIPSPPPC | 5–2,500 g | ±0.10–0.30 mm* | Required | Usually not required | Supplier declarations and periodic testing | Usually not required | Review color measurement method, appearance limit samples, warp controls, and packaging validation |
| Profile 04 | Bohai Economic Rim | Industrial equipment guards, covers, handles, and structural plastic assemblies | PA6 GFPOMPBTPC | 20–5,000 g | ±0.10–0.35 mm* | Required | Customer-specific | Compliance documentation available by material | Available for regulated programs | Verify load testing, insert-molding controls, maintenance records, and engineering-change procedure |
| Profile 05 | Yangtze River Delta | Medical-device housings, laboratory components, and clean-appearance parts | PCABSPOMPEEK | 1–1,200 g | ±0.05–0.20 mm* | Required | Usually not required | Material and chemical compliance review | Available when required by customer | Confirm cleanroom classification, biocompatibility responsibility, validation protocol, and lot traceability |
| Profile 06 | Central China | Large automotive trim, battery-system covers, ducts, and utility components | PP-TDTPOPA66 GFPPS | 500–12,000 g | ±0.20–0.60 mm* | Required | Preferred | REACH and RoHS evidence by bill of materials | Full submission package available | Assess machine tonnage, warpage simulation, weld-line strength, and sub-supplier controls |
| Profile 07 | Southwest China | Electrical connectors, cable-management parts, and flame-retardant components | PA66PBTPCLCP | 0.05–300 g | ±0.02–0.10 mm* | Required | Program-dependent | RoHS testing and REACH SVHC declarations | Available for automotive or industrial programs | Verify flame-retardant grade records, electrical testing, cavity balance, and terminal-fit capability |
| Profile 08 | Pearl River Delta | Optical, lighting, and transparent decorative components | PMMAPCSANABS | 0.5–1,500 g | ±0.05–0.25 mm* | Required | Usually not required | Material declarations and restricted-substance testing | Usually not required | Define haze, transmittance, gloss, weld-line, gate-mark, and scratch-acceptance criteria before tooling |
| Profile 09 | Yangtze River Delta | Overmolded grips, seals, tactile interfaces, and multi-material assemblies | TPETPUPPPC/ABS | 2–1,800 g | ±0.10–0.30 mm* | Required | Customer-specific | Declarations and supplier compliance records | Available where required | Check bonding tests, durometer control, insert positioning, cycle-time stability, and aging performance |
| Profile 10 | Northern China | Packaging closures, caps, dispensers, and high-volume commodity components | PPHDPELDPEPOM | 0.2–250 g | ±0.10–0.25 mm* | Required | Usually not required | Food-contact or restricted-substance documentation as specified | Usually not required | Confirm cycle capability, cavity-count consistency, leak testing, food-contact requirements, and recycled-content controls |
Choosing among China’s top ten plastic parts manufacturers requires more than comparing quoted prices. Lead time should include design review, mold fabrication, sampling, production, and export preparation. A supplier promising 15 days may exclude testing or port delays. Ask for a milestone schedule and inspect recent delivery records.
Tooling cost also needs careful review. A low mold quote can hide steel upgrades, maintenance, spare inserts, or engineering changes. Request a complete ownership statement, including cavity count, expected tool life, and repair responsibility. During sample approval, measure critical dimensions with calibrated equipment.
Defect rate should come from production data, not a sales promise. Confirm whether the figure covers cosmetic marks, warping, short shots, and rejected assemblies.
2024 CAGR can indicate market momentum, but it should not decide the purchase alone. A fast-growing supplier may still lack stable process control or enough technical staff. Compare audited revenue trends with capacity, equipment age, and customer concentration.
No scorecard is perfect. I have seen attractive reports fail during peak-season production. A small pilot order often reveals communication gaps, packaging weaknesses, and inconsistent color matching before a larger commitment. Record every assumption in the quotation, especially tolerance limits, inspection standards, tooling revisions, and acceptable defect levels.