How to Source Rubberized Dip Coating in 2026?
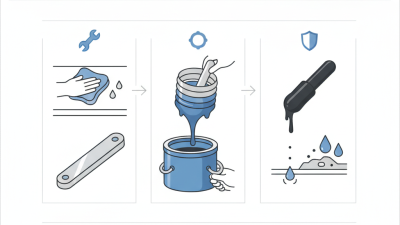
Sourcing rubberized dip coating in 2026 requires more than comparing prices on supplier websites. The coating must match the substrate, production method, and final-use environment. A flexible medical component needs different performance than a textured tool handle. Small differences matter.
Experienced buyers usually begin with a clear technical brief. It should define polymer type, hardness, thickness, color, surface texture, adhesion, and acceptable tolerances. Ask suppliers for recent technical data sheets, safety documentation, and representative samples. Check whether their testing methods match your application. A sample that feels excellent by hand may still fail after heat, oil, abrasion, or repeated bending.
Supplier credibility deserves careful attention. Review documented quality systems, production capacity, batch traceability, and customer references from comparable industries. Confirm how the factory controls viscosity, curing temperature, line speed, and coating thickness. Request a pilot run before approving full production. Keep inspection records, including photographs of surface defects and measurements from multiple points.
In 2026, responsible sourcing also includes material transparency and regional compliance requirements. Verify restricted-substance declarations, worker safety practices, packaging details, and waste-handling procedures. Requirements can change. Recheck them.
Do not rely on attractive samples alone. Color drift, pinholes, weak bonding, and inconsistent grip may appear later. We may not identify every risk during an initial audit. That limitation should be recorded honestly. A reliable sourcing plan combines technical evidence, factory communication, independent testing, and realistic contingency options. This approach supports consistent quality while reducing expensive surprises during scale-up.
Define 2026 Specifications: Shore A, ISO 37 Tensile, and Film Thickness
How to Source Rubberized Dip Coating in 2026?
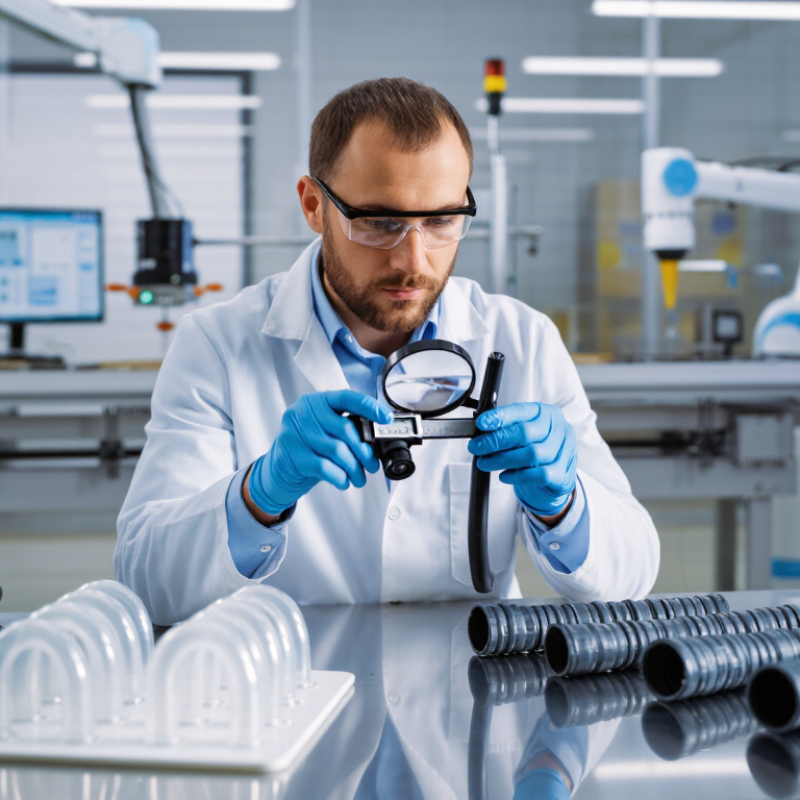
A reliable sourcing brief should define performance before discussing price. Shore A hardness is a starting point, not a complete specification. State the target value, tolerance, conditioning time, and test temperature. A coating measured at 70 Shore A may feel different after curing or aging. Ask suppliers to test finished parts, not only laboratory plaques.
Tensile performance should reference ISO 37 and identify the specimen type, conditioning conditions, tensile strength, and elongation targets. ISO 37 provides the test method, but it does not create a universal acceptance limit. Set requirements around the product’s real use. Flexible handles may need high elongation, while protective sleeves may require stronger tear resistance. Request raw data from several production lots. One attractive sample proves very little.
Film thickness needs equal attention. Specify the dry thickness range, measurement locations, and maximum variation between parts. Thin areas often appear near edges, corners, or hanging points. Use cross-section checks, calibrated gauges, or both. Define the acceptable range clearly, such as 0.80–1.20 mm, only after functional trials. Include adhesion, surface defects, curing evidence, and visual standards in the approval package. Small details matter. Supplier records should connect test results to lot numbers and production dates. A common mistake is approving a coating after one successful batch. Build a verification schedule instead, and revise the specification when field evidence challenges the original assumption.
Compare Rubber Compounds Using ASTM D573 Heat-Aging Data
How to Source Rubberized Dip Coating in 2026?
ASTM D573 heat-aging data can expose weaknesses hidden by fresh-condition testing. The standard commonly uses 70 hours at 100°C, although other temperatures and durations may apply. Compare tensile strength, elongation, and hardness before and after aging. A coating that retains 85% tensile strength deserves more attention than one showing only a strong initial result. Retention percentages matter.
A 2024 International Rubber Study Group market report placed global natural rubber demand near 15 million tonnes. That scale increases pressure on compound consistency, especially for dipped handles, seals, and protective sleeves. Ask suppliers for lot-specific ASTM D573 results, not a polished average. Check the test temperature, aging time, specimen thickness, and conditioning period. Missing details weaken the comparison.
Heat resistance is not the whole decision. A compound may retain strength but become noticeably harder, crack at a bend, or lose grip after aging. I have seen clean laboratory numbers fail to predict handling performance. That is uncomfortable, but useful. Request aged photographs, hardness changes, and repeat-test variation. ASTM D573 itself does not define one universal pass-or-fail limit; the buyer must set limits around the product’s real service temperature. Select the compound with balanced retention, stable processing, and documented batch control.
Qualify Suppliers Through ISO 9001, SPC, and ISO 2859 Sampling
How to Source Rubberized Dip Coating in 2026?
Qualify suppliers through ISO 9001, SPC, and ISO 2859 sampling. The ISO Survey 2023 recorded over 1.26 million ISO 9001 certificates worldwide. That figure shows broad adoption, not automatic coating quality. Ask suppliers for current certificates, scope details, audit findings, and corrective-action records. The certificate must cover production, not only office procedures.
Use SPC to examine compound viscosity, bath temperature, coating thickness, cure time, and adhesion. Request control charts from recent production lots. Check Cp and Cpk values, but do not accept attractive charts without raw data. In practice, one unexplained process shift can matter more than a polished capability report. Require traceable gauges and calibration records. A small weakness here is easy to miss.
Tips: Define an AQL under ISO 2859-1 before quoting. Specify lot size, inspection level, and critical defect rules. Sample rubberized parts from different cartons, not one convenient box. Test thickness, surface coverage, flexibility, and pull-off adhesion. Record failures with photos and batch numbers. The standard supports rational sampling, but it cannot replace engineering judgment. I would also run a pilot lot before approving regular supply. Supplier reviews often focus too much on paperwork. Real parts reveal more.
How to Source Rubberized Dip Coating in 2026?
Qualify Suppliers Through ISO 9001, SPC, and ISO 2859 Sampling
The chart shows single-sample sizes for normal inspection at General Inspection Level II under ISO 2859-1. Use the lot-size range to determine the minimum inspection quantity for incoming rubberized dip-coating lots. Combine sampling with ISO 9001 documentation, SPC records for coating thickness and adhesion, and approved acceptance criteria defined in the purchasing specification.